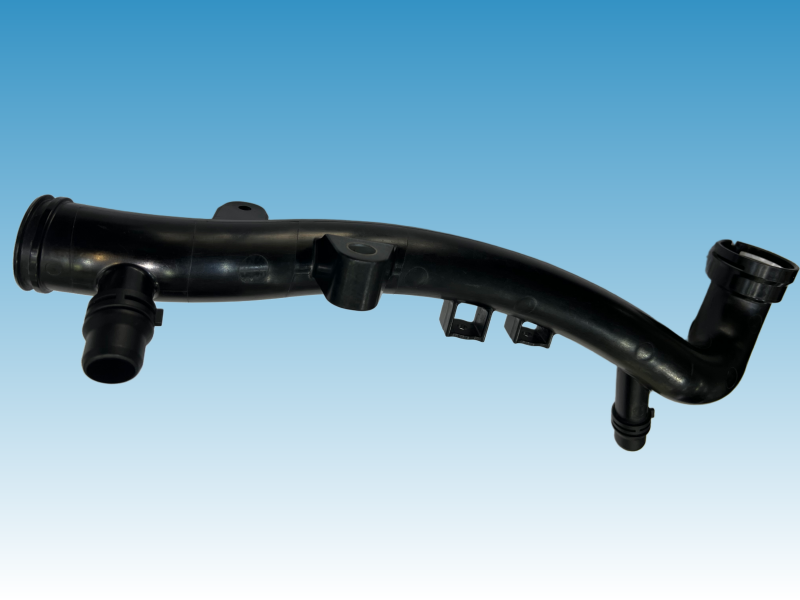
Gas Assisted Injection Molding: Process, Mold Design, Defects, and Alternatives
Process & Mold Design Guide · Gas Assist Injection · gasassistinjection.com
Gas-assisted injection molding uses nitrogen to create an internal pressurized channel that packs the part during cooling — cutting weight and preventing sink marks.
Many engineering teams search for “gas-assisted injection molding” when thick sections create sink marks, weight targets are tight, or conventional packing stops working once the gate freezes. GAIM addresses these challenges by injecting nitrogen into the still-molten polymer inside the mold cavity, creating an internal pressurized gas channel that supports packing during cooling and helps the surface skin solidify against the cavity wall.
GAIM isnotthe same as microcellular injection molding. GAIM forms a hollow channel by injecting gas after partial filling. Microcellular molding dissolves a supercritical fluid (typically N₂ or CO₂) into the melt and nucleates micro-bubbles when pressure drops in the mold. Each process suits different parts, and choosing the right one depends on your geometry, weight and surface goals.
In this article we walk through the GAIM process step by step, cover the mold and equipment requirements, review common defects and their practical fixes, and compare GAIM with microcellular molding so you can select the right technology for your part.
Gas Assisted Injection Molding (GAIM), also known as gas injection molding, is a process in which molten plastic is injected into a mold cavity — typically to a short-shot percentage — and then high-pressure nitrogen gas is injected into the polymer melt through a gas pin or nozzle. The gas displaces molten material in the core region, creating a hollow channel, while simultaneously acting like an internal packing force to compensate for volumetric shrinkage during cooling.
Reducepart weightby hollowing the core instead of packing it solid.
Reduceholding pressureand, in some cases, the requiredclamping force.
Improvedimensional stabilityin specific thick-wall geometries where uniform packing is difficult.
02 · Process
How the Process Works, Step by Step
Conventionally, plastic pellets are fed from a hopper into a rotating screw. The screw conveys, melts and homogenizes the polymer, then advances axially to inject the melt through the nozzle and runner system into the mold cavity. Gas-assisted molding modifies the later part of this cycle so that nitrogen, rather than additional plastic, completes the packing.
The four-stage GAIM cycle: partial fill → gas injection → gas packing → vent and eject.
Short-shot filling and switchover to gas
After the cavity is filled to a predetermined percentage, melt injection is stopped or reduced to a controlled switchover point. Pressurized inert gas is then introduced through the gas inlet according to a defined delay time and pressure profile. Getting the short-shot ratio right is critical: too little melt leaves the gas to search for a path and risks fingering; too much leaves no room for the hollow channel to form.
Gas penetration and internal packing
The gas preferentially travels through the hottest and least viscous region — typically the center of the melt flow. As it advances, it displaces the molten core, pushing the polymer outward toward the cavity walls. This forms a hollow channel while maintaining internal holding pressure that counteracts shrinkage during cooling. Because the gas stays mobile after the gate freezes, it can keep packing thick sections even when conventional plastic packing would stop.
Hollow channel control by gas outlet placement
By designing and positioning the gas outlet or overflow location, the hollow core can be directed and stabilized. This controls where the displaced melt flows, where the cavity forms, and how consistent the channel geometry remains across production. Gas channel layout and outlet placement are therefore design decisions made before the steel is cut.
03 · Approaches
Two Main Approaches in Gas Assisted Injection Molding
Depending on whether the goal is to create internal hollow channels or to improve surface definition, two approaches are commonly used.
Internal gas injection forms a hollow core; external gas injection consolidates the show surface against the mold.
Internal gas injection
Nitrogen is injected into the molten polymer within the component cavity to form a hollow core and maintain holding pressure from within. This is the most widely used method in GAIM: the gas follows the hottest, least viscous flow path, creating predictable hollow sections when the part design supports a continuous thick region.
External gas injection
Gas is applied to the outside surface of the component, still within the mold cavity, to consolidate the part against the mold surface. The gas forms a very thin layer between the mold core and the back surface of the part, helping the show surface more closely replicate the mold definition as the resin cools. This approach is used when surface replication matters more than weight reduction.
04 · System Requirements
Equipment and Mold Requirements
GAIM is a system solution. The mold and the gas control system determine repeatability — the machine alone is not enough.
GAIM is delivered by a coordinated system: nitrogen source, pressure control unit, gas pins, and a machine matched to the part.
Equipment requirements
Nitrogen sourceand gas generation or supply.
Injection molding machinecapable of the required shot control and clamp tonnage.
Gas pressure control unitfor injection pressure, holding pressure, timing, and safety logic.
Gas injection interface— gas pins, gas nozzles, or integrated hot-runner solutions.
Mold sealing and gas routingto keep gas where it is intended to go and to manage venting.
Mold requirements
Channel predictability is a geometry problem first.If the gas cannot find a consistent path, results drift — leading to uneven gas flow, incomplete filling, or localized weak spots.
Gate strategy must support the intended gas path.Normal packing stops once the gate freezes, but gas packing can keep applying pressure through the gas channel even after the gate is closed. Gate position and flow direction should keep the thick, sink-prone region connected to a steady gas path until the surface layer becomes firm.
Cooling balance prevents warpage even when the sink is solved.Gas packing transfers pressure efficiently, so shrinkage compensation can be achieved with less internal stress. But if one region freezes much earlier than another, uneven shrinkage forces still cause warpage even with gas packing.
Plan for venting and controlled gas release.When the mold opens, gas escapes through the air gap — treat it as a managed medium, not an afterthought.
05 · Applications
Common Applications
GAIM works best when the product design allows a stable hollow channel and the thick section is intentional and functional. Common categories include:
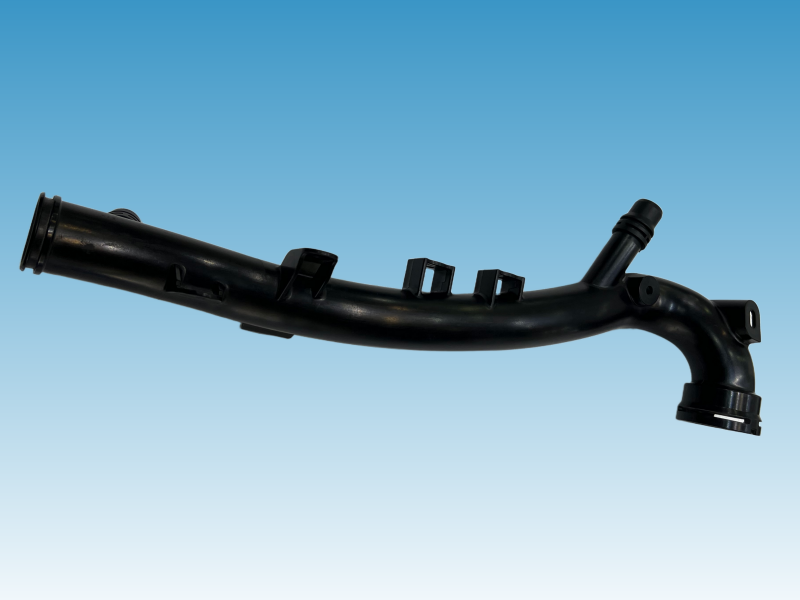
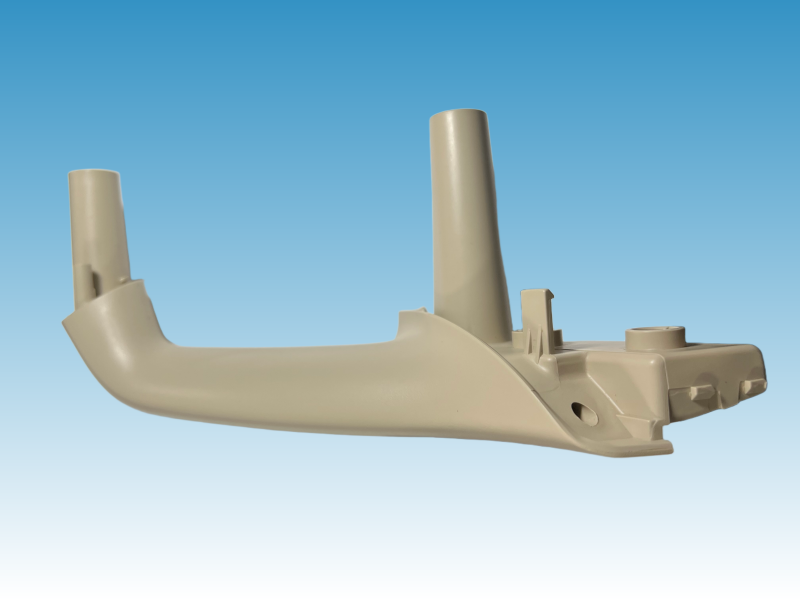
Handles and grip-like structures— door handles, tool handles, appliance handles.
Frames and beamswhere stiffness is needed but weight should be reduced.
Thick rib networkswhere sink must be controlled but a hollow core is acceptable.
Long, slender structural partsthat would warp or sink in conventional molding.
If your part has thick sections, long ribs, or strict weight and surface targets, GAIM is worth evaluating early in the design phase — before tooling is committed.
06 · Troubleshooting
Common Defects and Practical Fixes
Below are the defects most frequently discussed in GAIM engineering, along with the process knobs that typically influence them.
Blow through
Blow through happens when gas breaches the surface, leaving a rupture, whitening, or a visible surface defect. It is a risk when pressure or timing are not controlled.
What we check first:
Gas delay time and skin-formation window.
Peak gas pressure and ramp profile.
Wall thickness near the gas path.
Short-shot ratio and whether the cavity is overfilled before gas injection.
Gas fingering
Gas fingering is an unstable gas front that branches away from the intended channel, reducing stiffness and repeatability.
What we check first:
Whether the geometry forces the gas to split into competing paths.
Whether delay time and melt temperature create a melt core that is too mobile.
Whether the short-shot ratio leaves too much open volume for the gas to search.
Short fill or incomplete packing
This can happen if the short-shot percentage is too low, or if the gas holding pressure is insufficient to complete the fill consistently.
What we check first:
Fill percentage and injection-velocity profile.
Gas holding time and pressure stability.
Venting and air-trap locations.
07 · Technology Comparison
Gas Assisted Injection Molding vs. Microcellular Injection Molding
Although both processes use gas, their outcomes are fundamentally different.
What is microcellular injection molding?
Microcellular injection molding is a physical foaming process that incorporates a supercritical gas — typically nitrogen or carbon dioxide — into the molten polymer during injection. The gas dissolves under pressure, then microscopic bubbles nucleate when the mixture experiences a pressure drop in the mold. The result is a fine cellular structure across the part wall rather than a single hollow channel.
GAIM produces one defined hollow channel; microcellular molding creates fine micro-cells throughout the wall.
Key distinction between GAIM and microcellular molding
ChooseGAIMwhen the design has intentional thick sections, sink is the main concern, and a hollow channel is acceptable — for example handles, ribs and structural frames. Choosemicrocellular moldingwhen you want uniform low-density parts, thin-wall dimensional stability, or cycle-time savings across the whole part and can manage the resulting surface finish.
08 · FAQ
FAQ for Gas Assisted Injection Molding
What is the main purpose of GAIM?
GAIM primarily reduces sink marks and part weight on thick sections by using an internal nitrogen channel to pack the part during cooling, while lowering holding pressure and internal stress.
Is GAIM the same as microcellular injection molding?
Нет. GAIM injects gas after partial filling to create a hollow channel. Microcellular molding dissolves supercritical gas into the melt and nucleates micro-bubbles across the wall. They are different technologies with different outcomes.
What materials work well with GAIM?
Most thermoplastics respond well — PP, ABS, PA6/PA66, PC, PBT, PET, HDPE and PC/ABS blends are common. Materials with a broad molding window and predictable shrinkage behavior work best.
When should I consider microcellular injection molding instead?
Consider it for thin-wall parts, uniform dimensional stability, or cycle-time savings across the whole part — provided you can manage the surface finish. GAIM is usually the better choice when the design centers on thick, sink-prone sections.
09 · Conclusion
Conclusion: Lead With the Right Technology
Gas-assisted injection molding is a mature, proven way to produce lighter, sink-free, dimensionally stable parts when thick sections are part of the design. Its success, however, depends on the mold: gas channel layout, gate strategy, cooling balance and venting all have to be engineered together before the steel is cut.
AtГазовая инъекция с поддержкой, we design and manufacture high-precision molds for gas-assisted and conventional molding in our own factory — automotive, appliance and industrial applications. From design-for-manufacturability (DFM) to production, we help you select the right process and get parts right the first time.
Have a thick-wall or sink-prone part in mind?
Send your part geometry, material and intended application — we will review whether GAIM is right for your project and quote your mold and production scope.